
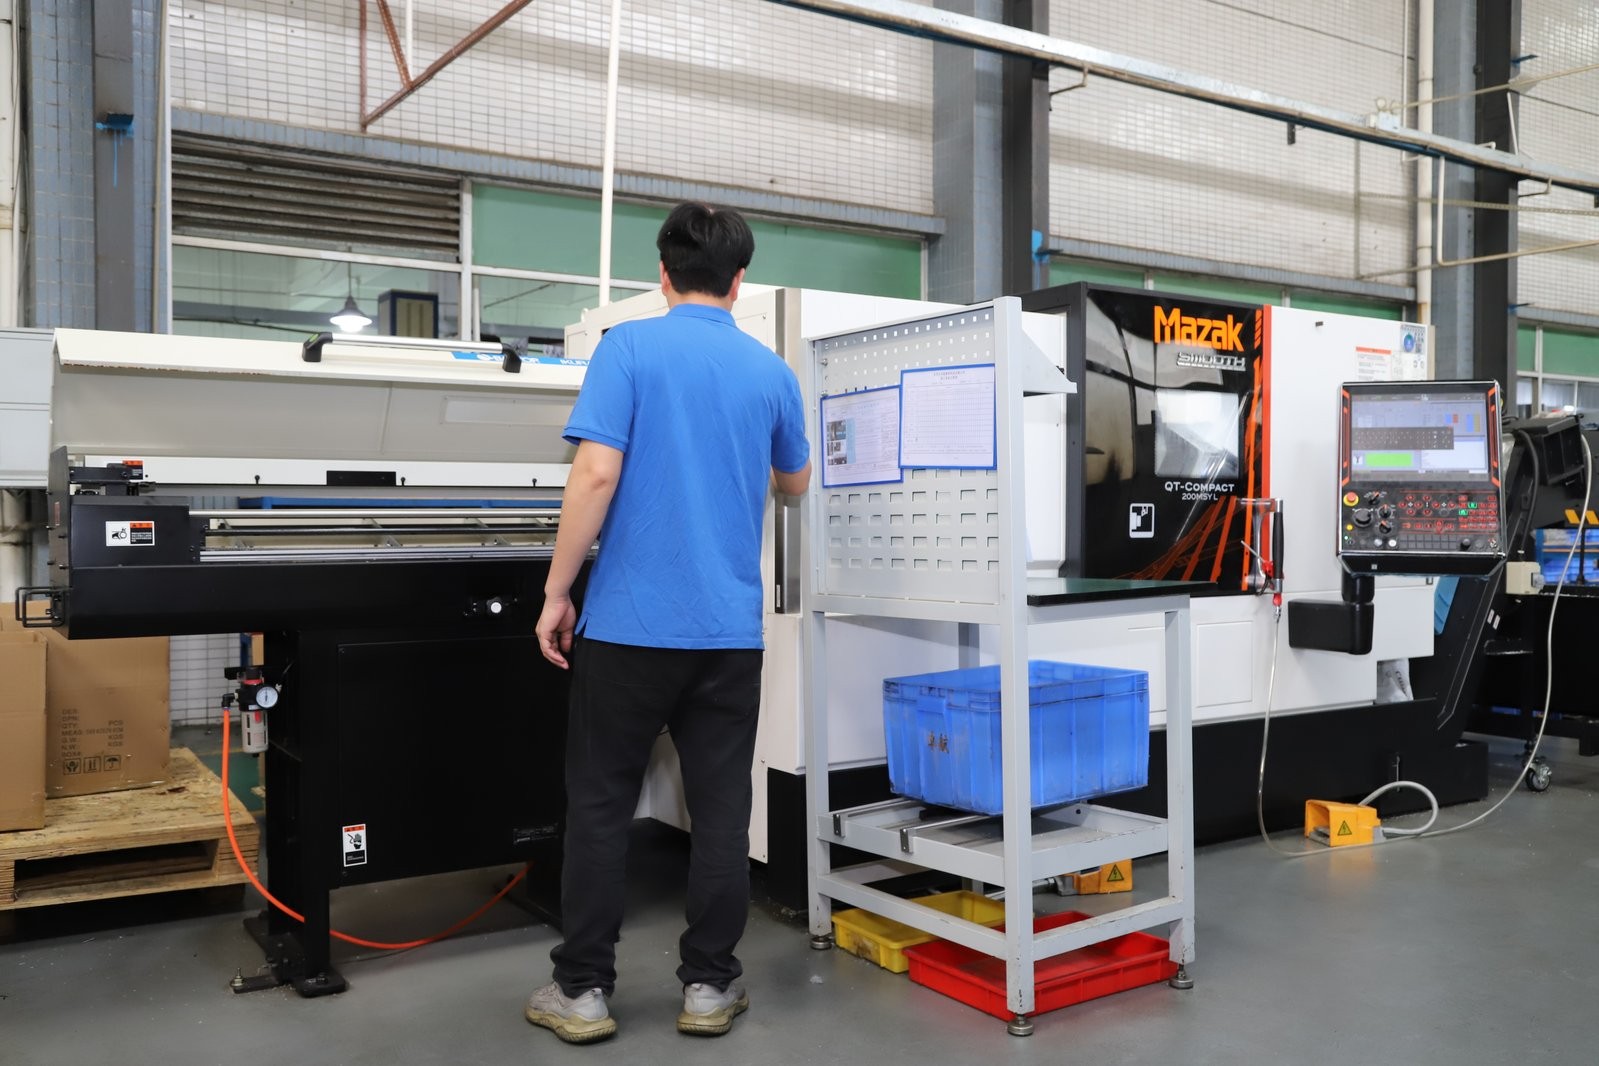
Which materials and industries do you cover?
We machine aluminum, stainless steel, titanium, brass, copper, and Inconel, plus engineering plastics including PEEK and Delrin. These Swiss turned parts go into medical, aerospace, automotive, robotics, electronics and defense applications, with the inspection, traceability and documentation each sector requires before it places an order.
What buyers ask most
Three questions come up on nearly every enquiry. What is the minimum order? One piece - a single prototype can be machined, checked and iterated before any volume is committed. What is the lead time? Roughly 3 / 7 / 30 days depending on the material and the documentation scope, from a simple aluminium part to a full first-article package. What tolerances can you hold? ±0.003 mm milled and ±0.002 mm turned, verified on a Hexagon CMM, with Ppk 1.67 or better initial and Cpk 1.33 or better in production on critical characteristics. The answers are short because the capability is specific, not vague.
The answers behind the answers
The plant behind these answers is Dongguan Zhuohang Ltd - 6,800 m² in Hengli Town, Dongguan, 100+ CNC machines including Mazak VARIAXIS I-600 and INTEGREX I-250H S, and certification to ISO 9001:2015, IATF 16949:2016 and ISO 14001:2015 with the certificate numbers published and verifiable. The service area covers Austria, Belgium, the Czech Republic, Denmark, France, Germany, Greece, Hungary, Ireland, Italy, the Netherlands, Spain, Sweden and the United Kingdom in Europe; Brazil, Canada, Mexico and the United States in the Americas; China, Israel, Japan, Singapore and Sri Lanka in Asia; Australia and New Zealand in Oceania; and South Africa in Africa, with worldwide shipping from Dongguan. Contact Felipe Iglesias at [email protected] or +86 13126536955 with a drawing and a quantity for a specific answer to your specific part.
What the floor can actually prove
Your next step
A drawing and a quantity are all it takes to turn this page into a real part. Send a STEP or IGES model plus a 2D drawing carrying the tolerances, datums, material grade and finish, and name the quantity and the lead time. That returns an itemised quote - material, setup, cycle time, inspection - instead of a round number. If the drawing is not done, send what exists and the questions holding you back; starting the conversation matters more than waiting for a perfect package.
Reach Felipe Iglesias at [email protected] or +86 13126536955. MOQ is 1 piece, lead times run roughly 3 / 7 / 30 days, and the service area covers Austria, Belgium, the Czech Republic, Denmark, France, Germany, Greece, Hungary, Ireland, Italy, the Netherlands, Spain, Sweden and the United Kingdom in Europe; Brazil, Canada, Mexico and the United States in the Americas; China, Israel, Japan, Singapore and Sri Lanka in Asia; Australia and New Zealand in Oceania; and South Africa in Africa, with worldwide shipping from Dongguan.
Tolerances and finishes, in one reference
Milling holds ±0.003 mm, turning ±0.002 mm, and grinding or wire EDM ±0.002 mm, each verified on a Hexagon CMM against the datum scheme on the drawing. Surface finishes run Ra 0.8 to 3.2 µm as-milled, Ra 0.2 to 0.4 µm ground, and Ra 0.05 to 0.1 µm polished. The 10:1 gauge rule applies to every feature - the instrument resolves ten times finer than the tolerance it checks. And a part is only as good as its datum: the same callout read against two different datums yields two different parts, so name the datum and the convention, ASME Y14.5 or ISO, on the drawing.
Choosing the right material
Aluminium 6061-T6 is the default light and economical pick; 7075-T6 adds strength for aerospace and structural work. Stainless 303 machines cleanly for fittings, 304 and 316 add corrosion resistance, and 17-4 PH gains strength after ageing. Steel is the strength-and-cost workhorse. Brass is the fastest metal to cut and conducts well. Copper C110 sets the conductivity benchmark, with C145 tellurium copper for machinability. Titanium and Inconel keep high-temperature strength but machine slowly and cost more. Material is the biggest lever on price, so choose it for the service - load, environment, temperature - not by habit, and name the grade on the drawing so the mill certificate confirms it.
Placing the part on the right process
The shortest way to a correct part is to let the shop read the drawing and place it on the right machine, because the process follows the geometry, the material and the tolerance - not the label on the page. A part with a turned profile goes to the lathe, a prismatic part to the machining centre, a long thin part to a Swiss machine, and a sheet or panel to the router; you state what the part must do, and the shop matches the process. That is the whole of the routing decision, and it is settled at the quote.
This floor runs 100+ CNC machines - Mazak VARIAXIS I-600 five-axis, Mazak INTEGREX I-250H S mill-turn, Brother SPEEDIO, and TSUGAMI, STAR and CITIZEN Swiss lathes - at ±0.003 mm milled and ±0.002 mm turned, verified on a Hexagon CMM, with certification to ISO 9001:2015, IATF 16949:2016 and ISO 14001:2015. MOQ is 1 piece and lead times run roughly 3 / 7 / 30 days. Send the drawing to Felipe Iglesias at [email protected] or +86 13126536955 and the process is matched to the part.
How the quality system works
No part leaves this floor without evidence. Incoming stock is checked against the mill certificate - composition by XRF, hardness where specified - before it is cut. The first article is inspected in full against the drawing, and critical characteristics run under statistical process control at Ppk 1.67 or better initial and Cpk 1.33 or better in production. In-process inspection holds tolerance on a Hexagon CMM with the 10:1 gauge rule, and the final report ships with the parts, so the product and the proof arrive together. That is what separates a tolerance that is held from one that is claimed.
Reading a quote like a buyer
A quote is only as good as the drawing behind it. Name the material grade, not just the material; mark the datums and tolerances that actually matter; state the finish you need; and give a quantity, even a range. The more the drawing specifies, the less the shop assumes, and the closer the quote lands to the real part. An itemised quote - material, setup, cycle time, inspection - lets you challenge the right line instead of negotiating blind, and it is the fastest route to a cheaper part: loosen a tolerance that does not matter, or raise the quantity to spread the setup. Send the drawing to Felipe Iglesias at [email protected] or +86 13126536955 and ask for it itemised.
De-risking a first order
If this is a first order, a small trial run is the cheapest way to de-risk: a few parts shipped with the drawing and the inspection report, so the routing, the tolerance and the documentation are proven before volume commits. The same floor, the same CMM and the same certificates cover one piece and a thousand alike, so the trial result carries straight into the production run.
What this shop actually runs
Ask for capability evidence and the answer should be specific. The facility behind this guide runs 100+ CNC machines on a 6,800 m2 floor in Dongguan, China, with 100+ staff. The machine list, by category:
- 5-axis machining centres (10+) - Mazak VARIAXIS I-600 (510/910/510 mm travel, 12,000 rpm, 22 kW, 71.6 N·m, 30-tool BT40) and Mazak INTEGREX I-250H S (B-axis 0.0001°, 24 kW, 124 N·m, 38-tool HSK-A63). Set up for compound-angle parts, single-setup multi-face prismatic work, and aerospace fittings where datum transfer loss is unacceptable.
- 3-axis / 4-axis machining centres (50+) - Brother SPEEDIO S500Z2N / S700Z2N (10,000 rpm, 14/21-tool ATC, 0.7 s tool-to-tool, Z-axis 2.2 G) and Mazak VCE-430A L / VCE-570C L (10,000 rpm, 118 N·m, 24-tool ATC). Set up for prismatic parts, plates, brackets, housings.
- Swiss-type turning centres (10+) - Citizen Cincom A20-3F7 (Φ20 mm, 10,000 rpm), TSUGAMI B0206-III / B0205-III (Φ20 mm, 0.1 µm), STAR SR-32JII / SR-32J Type N (Φ32 mm, 8,000 rpm). Set up for long, slender rotational parts at ±0.002 mm.
- CNC turning centres (20+) - HEADMAN T70M/1250 (720 mm swing, 117 mm bore, 3,000 rpm, BMT75 12-station turret). Set up for shafts, bushings, flanges up to ±0.002 mm.
- Wire EDM (5+) - Sodick AQ535L (550/350/300 mm travel, ±20° taper, 800 kg workpiece). Set up for hardened tool steel, internal splines, sharp internal corners that milling cannot reach.
- Inspection: Hexagon CMM + 20+ gauges - Hexagon CMM for coordinate measurement, plus vision system, profilometer, hardness tester, coating thickness gauge, XRF for material verification. The 10:1 rule (gauge 10x more accurate than the band) is applied to every feature.
- Machine highlights - VARIAXIS I-600: one-setup multi-face 5-axis + MAZA-CHECK auto-calibration; INTEGREX I-250H S: DONE-IN-ONE mill-turn, B-axis 0.0001° + Ai thermal shield; SPEEDIO S500Z2N / S700Z2N: Z-axis 2.2 G + 0.7 s ATC; Swiss-type: guide-bush switchable + 0.1 µm resolution.
Tolerances held: milling ±0.003 mm, turning ±0.002 mm, grinding and wire EDM ±0.002 mm. Capability: Ppk >= 1.67 initial and Cpk >= 1.33 in production on key characteristics.
Certifications: ISO 9001:2015 (116024/A/0001/UK/En), IATF 16949:2016 (131941/A/0001/SM/En, clause 8.3 design excluded, disclosed openly) and ISO 14001:2015 (116024/B/0001/UK/En), issued to Dongguan Zhuohang Ltd, USCC 91441900MA4UWT6X39, established 2005.
Service area: Austria, Belgium, the Czech Republic, Denmark, France, Germany, Greece, Hungary, Ireland, Italy, the Netherlands, Spain, Sweden and the United Kingdom in Europe; Brazil, Canada, Mexico and the United States in the Americas; China, Israel, Japan, Singapore and Sri Lanka in Asia; Australia and New Zealand in Oceania; and South Africa in Africa — built in China, shipped worldwide.
Contact: Felipe Iglesias, [email protected], +86 13126536955.
Have a question this page did not cover?
Email [email protected] or call +86 13126536955 for a direct answer.
Frequently Asked Questions
Why does material-to-process matching matter for turned parts?
In short, The material decides how fast you can cut, how long the tool lasts, and whether the tolerance holds as heat builds. Matching the alloy to the right machine and process is what keeps a ±0.002 mm (turning) / ±0.003 mm (milling) dimension from becoming a hope instead of a fact.
Which materials suit Swiss-type lathes best?
Free-machining grades cut cleanest on Swiss-type lathes: 303 stainless, 12L14 steel, C360 brass, and 2011 aluminum break chips and hold size on long, slender shafts. Demanding alloys like 316 or titanium turn slower and cost more.
How does stainless steel grade choice affect the process?
303 is the free-machining cousin of 304 — sulfur added to break chips makes it cut cleanly on a Swiss lathe. 316 and 17-4PH work-harden and gall more, so they turn slower and wear inserts faster, pushing up cost and lead time.
How is titanium matched to a process?
Titanium conducts heat poorly and springs back after cutting, so it needs rigid machines, sharp tools, and slower feeds. Stress relief above 500 °C is outsourced because the in-house ovens cap at 500 °C — a material-process fact stated honestly.
When does grinding enter the material-process match?
Grinding enters when a dimension needs ±0.002 mm or a fine surface finish that turning alone cannot reach. Surface, centerless, and cylindrical grinding finish bearing seats and roundness-critical surfaces.
How does the material affect lead time?
Free-machining materials run fast and ship in the shorter 3 or 7-day tiers. Demanding alloys and any surface finishing push a part toward the 30-day tier, so the material choice is also a schedule choice.
1. Which materials and industries do you cover?
In short, We machine aluminum, stainless steel, titanium, brass, copper, and Inconel, plus engineering plastics including PEEK and Delrin. These Swiss turned parts go into medical, aerospace, automotive, robotics, electronics and defense applications, with the inspection, traceability and documentation each sector requires before it places an order.
What is the diameter range for Swiss turning?
In short, Swiss-type lathes here cover small, long, thin parts in the range where a guide bushing holds the bar next to the tool, which is exactly the geometry a conventional lathe struggles with. The TSUGAMI B0206-III/B0205-III and Citizen Cincom A20-3F7 run that work.
Why does Swiss turning beat conventional turning on long thin parts?
In short, The guide bushing supports the bar right at the cut, so a long, small-diameter part does not deflect the way it does when it hangs out of a fixed-head chuck. That is how a Swiss part holds ±0.002 mm over a length a conventional lathe would spring on.
What tolerance do you hold on Swiss parts?
±0.002 mm on turned diameters, verified on a Hexagon CMM, with Ppk 1.67 initial and Cpk 1.33 in production on the critical features. A Swiss part is small, but the tolerance discipline is the same as a large one.
What payment methods and terms do you accept?
PayPal, Western Union, and bank or wire transfer. For long-term customers we also accept Net 30, Net 45, and Net 60 terms after an approved credit review.
What happens if a machined part has a manufacturing defect?
We provide free repair or remake for parts with manufacturing defects. All repair and remake costs, including return and shipping, are on us.
How quickly do you respond to inquiries?
We respond to every inquiry within 24 hours. Quotations for standard parts are returned within 48 hours; print reviews and DFM feedback are usually back within one business day.
Standards referenced on this page
- ASTM A276/A276M-17 — Standard Specification for Stainless Steel Bars and Shapes
- ASTM A582/A582M-12 — Standard Specification for Free-Machining Stainless Steel Bars
- ISO 9001 — Quality management systems — Requirements