
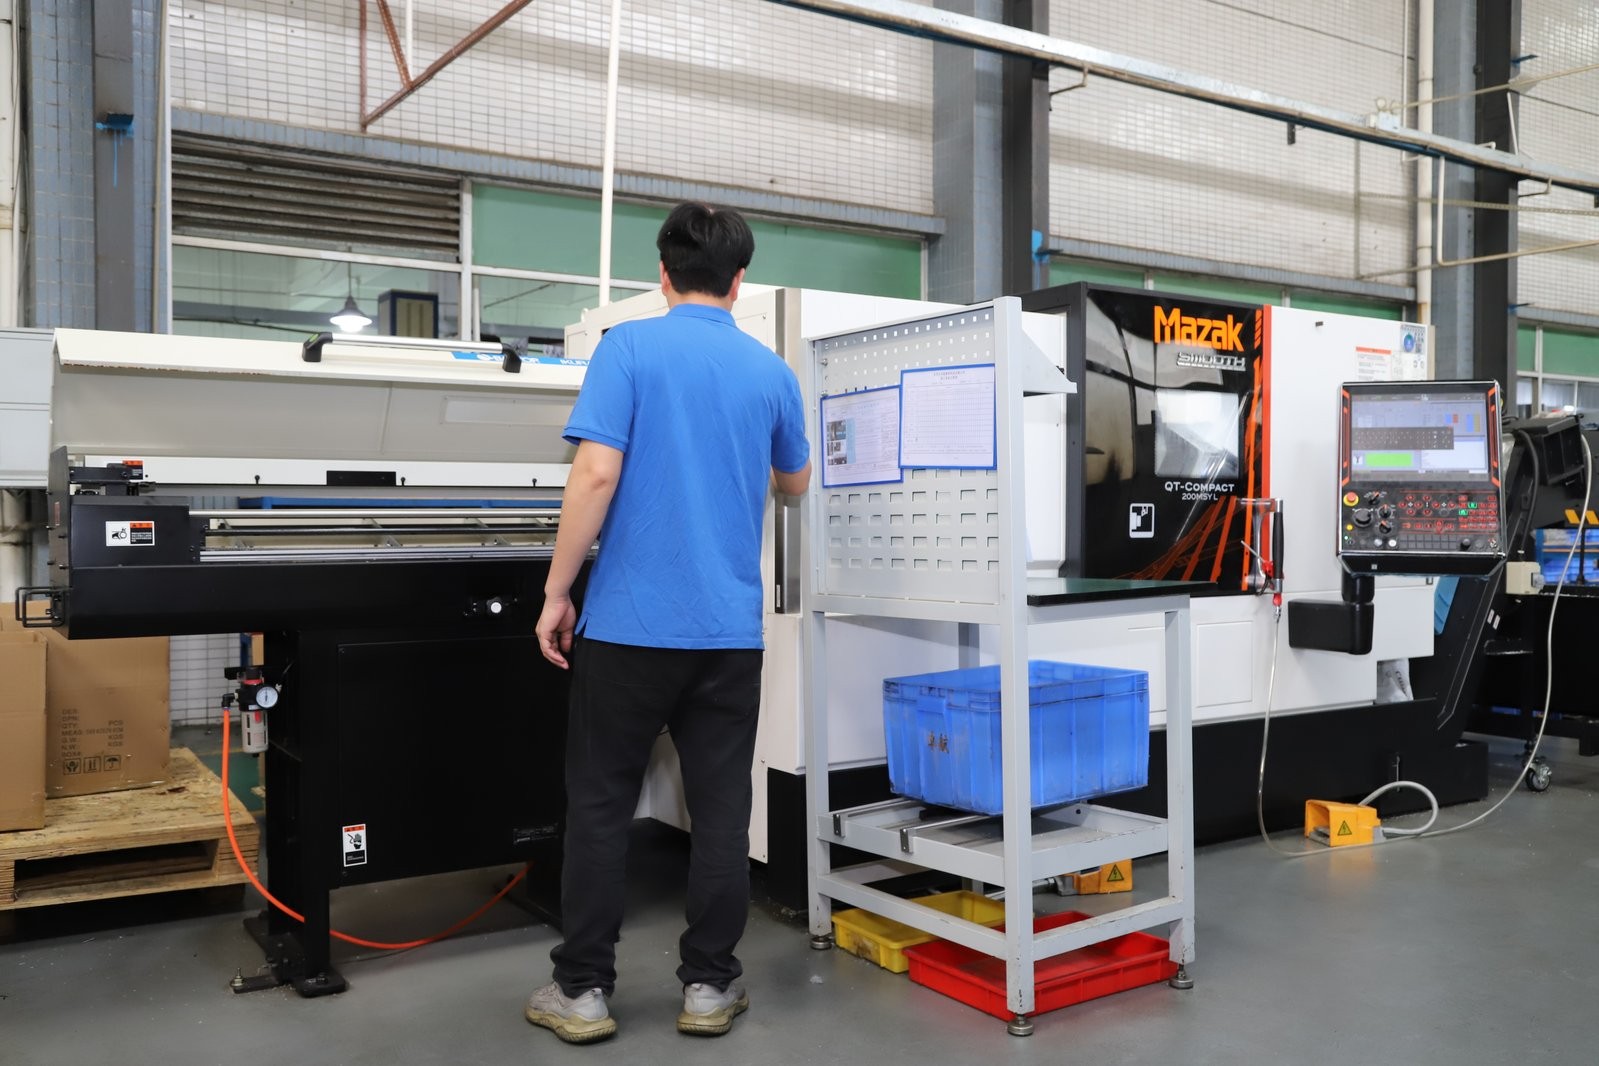
- 6,800 m² across two buildings in Hengli Town, Dongguan, production, inspection, and engineering under one roof.
- ISO 9001:2015 / IATF 16949:2016 / ISO 14001:2015, certificate numbers published and verifiable.
- Multi-axis Machining: Parts whose critical surfaces are curved or whose features are distributed around more than one datum.
- Where it stops: More axes means more collision cases to verify offline.
- Prototype and production run on the same floor and the same process.
How multi-axis machining works, in engineering terms
Multi-axis machining is a machine that can move the tool and the workpiece through more than three axes in a controlled, simultaneous way.
The distinction that matters is between indexing — where the rotary axes lock while cutting happens — and simultaneous motion, where all axes interpolate together. Simultaneous motion is what produces a continuous surface on an impeller blade; indexing is what keeps a clocked hole pattern cheap.
How do you verify a supplier really has this capability?
Ask whether the programmes are verified by simulation before release, and ask to see the collision report. On multi-axis work the number of collision cases grows with each rotary axis, and a supplier that cannot show you how it checks them is guessing.
None of these questions are hostile and all of them are cheap. A plant with the capability answers them easily; a brochure cannot.
Three things that change the price without changing the part
On multi-axis work the hidden cost is verification time. Every additional rotary axis multiplies the collision cases that have to be simulated before the programme is released, so geometry that forces the head into an awkward attitude is expensive even when it cuts quickly. Where a feature can be reached with the head upright, leaving it upright is worth real money.
This should come up when quoting, before any metal is cut, because the changes are usually trivial on the drawing and significant on the machine.
What identifies the legal entity behind the machines?
The registered entity is Dongguan Zhuohang Ltd, China Social Credit Code 91441900MA4UWT6X39, established 2005, also known as Zhuohang Precision Machining Factory. Registered and production address: No. 8, Shuibian Songyuan Road, Hengli Town, Dongguan, Guangdong, China 523470.
You can verify a Chinese manufacturer through the National Enterprise Credit Information Publicity System with that 18-character code. A trading company can also produce a business licence, but it shows a trading scope rather than manufacturing, and an office address rather than a plant.
How much capacity sits behind it?
over a hundred machines with depth in every relevant family — 50+ three-axis, 20+ four-axis, 20+ five-axis, 25+ turning centres, plus Swiss-type, grinding, and wire EDM.
Where does multi-axis machining pay off on swiss machining?
Parts whose critical surfaces are curved or whose features are distributed around more than one datum.
Rates rise with axis count, but the saving appears in fixture count and in the number of times a part is handled.
What multi-axis machining cannot do
More axes means more collision cases to verify offline. Simulation is not optional, and that verification time belongs in the quote.
This boundary is stated deliberately. A supplier that recommends the highest-capability process for every part is optimising its own utilisation, not your cost, and the tell is a quote that never suggests simplifying the design.
What does the setup cost, and when is it worth it?
Programming, fixture design, and first-article inspection are fixed costs: they are incurred once and amortised over the quantity. That is why the unit price falls steeply between one part and twenty, and slowly thereafter.
The practical consequence is that a fixture worth building for fifty parts is not worth building for two, and a supplier that quotes the same unit price at both quantities has not thought about how it will hold the part.
Which standards the plant is certified to
Three certificates, each with a number you can check with the registrar: ISO 9001:2015 (116024/A/0001/UK/En), IATF 16949:2016 (131941/A/0001/SM/En), and ISO 14001:2015 (116024/B/0001/UK/En).
The IATF 16949 certificate excludes clause 8.3 (product design). That is normal for a build-to-print manufacturer and it is stated here rather than left for an auditor to discover: we cut to the drawings you provide, it does not originate the design.
What tolerance applies?
±0.003 mm on CNC milling, ±0.002 mm on CNC turning; ±0.002 mm where precision grinding or wire EDM is used, fixed for each feature at the quote.
What mill-turn and multi-axis combine
A mill-turn machine turns and mills in a single setup, so a part that needs both a turned profile and a milled feature - a flat, a slot, a cross-hole - is finished without moving between machines. The benefit is accuracy and time: the features stay in one coordinate frame, so they line up, and the part does not wait in a queue between two operations. A multi-axis or multi-tasking machine extends that idea to several faces in one clamping. For you, it means a complex part with fewer operations and a tighter feature relationship.
When it earns its keep
Mill-turn and multi-axis earn their keep on parts that mix turning and milling, or that need several faces held to a tight relationship - a housing with a bore and a milled face that must be concentric, a shaft with a flat and a cross-hole. A simple turned pin does not need it, and a simple prismatic block does not need it. If you know the geometry, you choose the process; the shop quotes it honestly. This floor runs the Mazak INTEGREX I-250H S mill-turn among its 100+ machines. Contact Felipe Iglesias at [email protected] or +86 13126536955 with the drawing.
What the floor can actually prove
Behind the numbers is a floor you can walk. Dongguan Zhuohang Ltd runs 100+ CNC machines - the Mazak VARIAXIS I-600 five-axis, the INTEGREX I-250H S mill-turn, Brother SPEEDIO, and TSUGAMI, STAR and CITIZEN Swiss lathes - across 6,800 m² in Hengli Town, Dongguan. Every critical feature is checked on a Hexagon CMM under the 10:1 gauge rule, and the certificate numbers for ISO 9001:2015, IATF 16949:2016 and ISO 14001:2015 are published and verifiable. Capability is tracked with Ppk 1.67 or better at the initial study and Cpk 1.33 or better in production, which is the difference between a tolerance that is quoted and a tolerance that is held.
The same floor serves buyers worldwide - Austria, Belgium, the Czech Republic, Denmark, France, Germany, Greece, Hungary, Ireland, Italy, the Netherlands, Spain, Sweden and the United Kingdom in Europe; Brazil, Canada, Mexico and the United States in the Americas; China, Israel, Japan, Singapore and Sri Lanka in Asia; Australia and New Zealand in Oceania; and South Africa in Africa - with shipping from Dongguan. MOQ is 1 piece and lead times run roughly 3 / 7 / 30 days depending on material and documentation. Send the drawing and the quantity to Felipe Iglesias at [email protected] or +86 13126536955, and the quote comes back with the process behind it.
Your next step
A drawing and a quantity are all it takes to turn this page into a real part. Send a STEP or IGES model plus a 2D drawing carrying the tolerances, datums, material grade and finish, and name the quantity and the lead time. That returns an itemised quote - material, setup, cycle time, inspection - instead of a round number. If the drawing is not done, send what exists and the questions holding you back; starting the conversation matters more than waiting for a perfect package.
Reach Felipe Iglesias at [email protected] or +86 13126536955. MOQ is 1 piece, lead times run roughly 3 / 7 / 30 days, and the service area covers Austria, Belgium, the Czech Republic, Denmark, France, Germany, Greece, Hungary, Ireland, Italy, the Netherlands, Spain, Sweden and the United Kingdom in Europe; Brazil, Canada, Mexico and the United States in the Americas; China, Israel, Japan, Singapore and Sri Lanka in Asia; Australia and New Zealand in Oceania; and South Africa in Africa, with worldwide shipping from Dongguan.
Tolerances and finishes, in one reference
Milling holds ±0.003 mm, turning ±0.002 mm, and grinding or wire EDM ±0.002 mm, each verified on a Hexagon CMM against the datum scheme on the drawing. Surface finishes run Ra 0.8 to 3.2 µm as-milled, Ra 0.2 to 0.4 µm ground, and Ra 0.05 to 0.1 µm polished. The 10:1 gauge rule applies to every feature - the instrument resolves ten times finer than the tolerance it checks. And a part is only as good as its datum: the same callout read against two different datums yields two different parts, so name the datum and the convention, ASME Y14.5 or ISO, on the drawing.
What this shop actually runs
Ask for capability evidence and the answer should be specific. The facility behind this guide runs 100+ CNC machines on a 6,800 m2 floor in Dongguan, China, with 100+ staff. The machine list, by category:
- 5-axis machining centres (10+) - Mazak VARIAXIS I-600 (510/910/510 mm travel, 12,000 rpm, 22 kW, 71.6 N·m, 30-tool BT40) and Mazak INTEGREX I-250H S (B-axis 0.0001°, 24 kW, 124 N·m, 38-tool HSK-A63). Set up for compound-angle parts, single-setup multi-face prismatic work, and aerospace fittings where datum transfer loss is unacceptable.
- 3-axis / 4-axis machining centres (50+) - Brother SPEEDIO S500Z2N / S700Z2N (10,000 rpm, 14/21-tool ATC, 0.7 s tool-to-tool, Z-axis 2.2 G) and Mazak VCE-430A L / VCE-570C L (10,000 rpm, 118 N·m, 24-tool ATC). Set up for prismatic parts, plates, brackets, housings.
- Swiss-type turning centres (10+) - Citizen Cincom A20-3F7 (Φ20 mm, 10,000 rpm), TSUGAMI B0206-III / B0205-III (Φ20 mm, 0.1 µm), STAR SR-32JII / SR-32J Type N (Φ32 mm, 8,000 rpm). Set up for long, slender rotational parts at ±0.002 mm.
- CNC turning centres (20+) - HEADMAN T70M/1250 (720 mm swing, 117 mm bore, 3,000 rpm, BMT75 12-station turret). Set up for shafts, bushings, flanges up to ±0.002 mm.
- Wire EDM (5+) - Sodick AQ535L (550/350/300 mm travel, ±20° taper, 800 kg workpiece). Set up for hardened tool steel, internal splines, sharp internal corners that milling cannot reach.
- Inspection: Hexagon CMM + 20+ gauges - Hexagon CMM for coordinate measurement, plus vision system, profilometer, hardness tester, coating thickness gauge, XRF for material verification. The 10:1 rule (gauge 10x more accurate than the band) is applied to every feature.
- Machine highlights - VARIAXIS I-600: one-setup multi-face 5-axis + MAZA-CHECK auto-calibration; INTEGREX I-250H S: DONE-IN-ONE mill-turn, B-axis 0.0001° + Ai thermal shield; SPEEDIO S500Z2N / S700Z2N: Z-axis 2.2 G + 0.7 s ATC; Swiss-type: guide-bush switchable + 0.1 µm resolution.
Tolerances held: milling ±0.003 mm, turning ±0.002 mm, grinding and wire EDM ±0.002 mm. Capability: Ppk >= 1.67 initial and Cpk >= 1.33 in production on key characteristics.
Certifications: ISO 9001:2015 (116024/A/0001/UK/En), IATF 16949:2016 (131941/A/0001/SM/En, clause 8.3 design excluded, disclosed openly) and ISO 14001:2015 (116024/B/0001/UK/En), issued to Dongguan Zhuohang Ltd, USCC 91441900MA4UWT6X39, established 2005.
Service area: Austria, Belgium, the Czech Republic, Denmark, France, Germany, Greece, Hungary, Ireland, Italy, the Netherlands, Spain, Sweden and the United Kingdom in Europe; Brazil, Canada, Mexico and the United States in the Americas; China, Israel, Japan, Singapore and Sri Lanka in Asia; Australia and New Zealand in Oceania; and South Africa in Africa — built in China, shipped worldwide.
Contact: Felipe Iglesias, [email protected], +86 13126536955.
Ask the four questions before you commit
Registration number, machine depth, certificate numbers, and a walk of the floor. Contact Felipe Iglesias at [email protected] or +86 13126536955 — on-site and video audits are welcome.
Frequently Asked Questions
How is an engineering change handled mid-production?
The change is documented against a revision, the affected parts in process are identified, and the revised drawing is confirmed in writing before work restarts. The important part is that the revision in force at any moment is a single, written one.
How is material traceability maintained?
Incoming stock is checked against the mill certificate — composition by XRF, hardness where specified — and traceability is held per heat or per batch as the certificate defines it.
Is multi-axis always better than fewer axes?
In short, No. More axes means more collision cases to verify offline.
Are you a manufacturer or a trading company?
A manufacturer. The legal entity is Dongguan Zhuohang Ltd (Registration No. 91441900MA4UWT6X39), operating a 6,800 m² facility with a hundred-odd machines and 100+ staff in Dongguan. Factory visits are welcome.
What parts suit multi-axis work best?
Parts whose critical surfaces are curved or whose features are distributed around more than one datum. On the wrong geometry the extra axes cost programming time and buy nothing.
Which markets do you export to?
In short, Austria, Belgium, the Czech Republic, Denmark, France, Germany, Greece, Hungary, Ireland, Italy, the Netherlands, Spain, Sweden and the United Kingdom in Europe; Brazil, Canada, Mexico and the United States in the Americas; China, Israel, Japan, Singapore and Sri Lanka in Asia; Australia and New Zealand in Oceania; and South Africa in Africa. Our service area also spans Europe, the Americas, Asia, Oceania and Africa — based in China, we serve customers worldwide.
What happens if the first article does not conform?
In short, The nonconformance is documented and the corrective action is agreed before any further parts are made. Whether the replacement cost sits with the plant or the customer depends on where the deviation came from, which is why the revision and the drawing standard are confirmed in writing at the start.
Continue reading: 3 Axis Swiss Machining · 4 Axis Swiss Machining · 5 Axis Swiss Machining
Standards referenced on this page
- ASTM A582/A582M-12 — Standard Specification for Free-Machining Stainless Steel Bars
- ISO 9001 — Quality management systems — Requirements
- ASTM E8/E8M-21 — Standard Test Methods for Tension Testing of Metallic Materials